Introduction: The Core Cornerstone of High-Quality PVC Products
From durable pipes and sturdy window frames to complex cable insulation materials, rigid polyvinyl chloride (PVC) is the cornerstone of modern industry. However, the production of these high-performance terminal products did not begin with ready to use materials, but with fine raw powders. This raw PVC powder itself is not suitable for direct processing - it lacks stability, fluidity, and the necessary properties required for molding. Transforming this powder into high-quality, homogeneous, and processable particles is not just a step, but a critical link that determines the quality, efficiency, and success or failure of the entire downstream manufacturing process.
Why PVC Compounding Pelletizing Necessary?
Why is it crucial to convert PVC powder and additives into pellets?
* Homogeneity and Precision: The original PVC powder is like a piece of white paper. To make it a functional material, it is necessary to accurately mix multiple additives - heat stabilizers, lubricants, impact modifiers, fillers, and pigments. Simply mixing these powders is not enough. The compounding process ensures that each pellet is a perfectly homogenized micro-formulation. This ensures consistent color, mechanical properties, and thermal stability in the final product, eliminating defects and variations.
* Processability and Efficiency: The powder is difficult to handle and needs to be continuously fed into the extruder, and it is prone to generating dust. On the other hand, pellets designed with special processes to be easy to flow, they can smoothly and reliably enter processing equipment such as pipeline extruders or profile extruders, ensuring the stability and continuity of the production process. This directly translates into higher output, less downtime, and lower operating costs.
* Improved Performance: The compounding process is more than just mixing; it's a chemical and physical fusion. Under the heat and shear of the extruder, additives are not only mixed but also molecularly bonded to the PVC resin. This creates a compound with superior properties—higher impact strength, improved weather resistance, and a longer service life—that far exceed what can be achieved with simple dry blending.
* Storage, Handling, and Safety: Pellets are clean, dense and easy to store and transport. They significantly reduce the health and safety risks associated with airborne PVC powder dust, creating a safer working environment.
Three key elements: in-depth analysis of the optimal pelletizing process
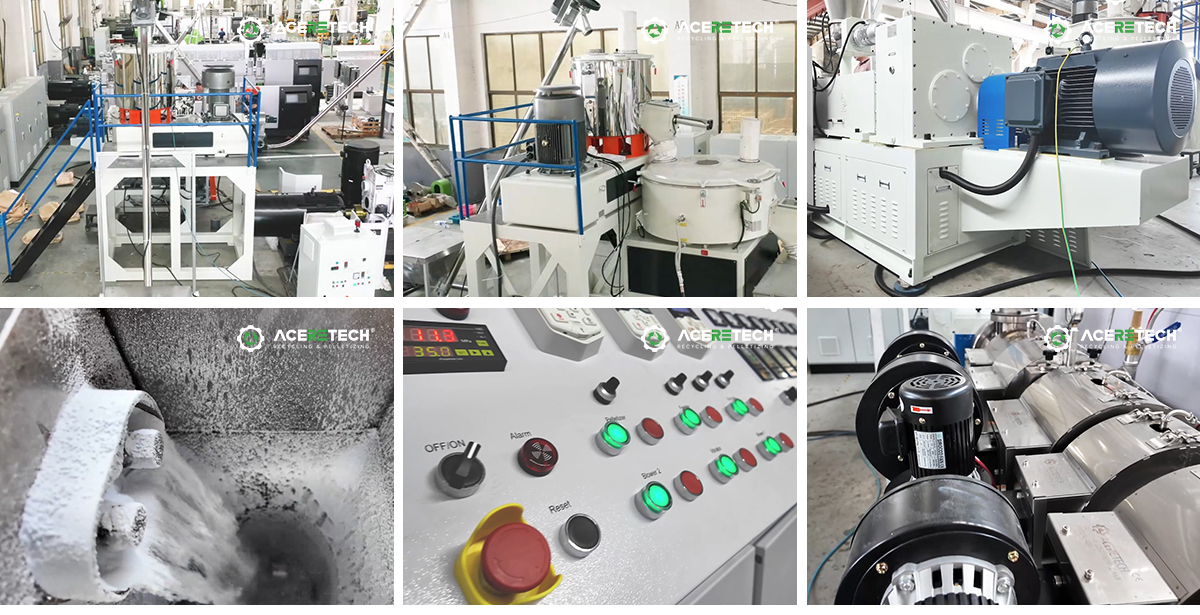
As shown in our video, the most efficient and reliable method for producing high-quality PVC compounds involves a three-stage system: high-speed mixer (hot mixing and cold mixing integrated machine), conical twin-screw extruder, and air-cooling die face hot cutting system.
Stage 1: High-Speed Mixer (Hot and Cold Mixer)—Perfect Premixing
The process begins in the high-speed mixer. Here, the raw PVC powder and all additives are added.
* Hot Mixing: The high-speed mixer generates physical shear and frictional heat through high-speed rotation, enabling PVC and various additives to undergo a transition from "physical mixing" to "physical chemical mixing" at a specific temperature, providing a uniform and stable "dry mix" for the production of high-quality PVC products.
* Cold Mixing: The hot mixed material will be automatically discharged into the cold mixer. During this process, the material can be quickly cooled to room temperature while still being mixed at a lower speed. This step can prevent material clumping and stabilize the quality of dry mixed materials. These two steps are crucial for achieving stable feeding and the quality of the final product.
Stage 2: Conical Twin-Screw Extruder—The Heart of Compounding
Perfectly premixed powders are fed into the conical twin-screw extruder, the heart of the entire operation. Why are conical twin-screws preferred for rigid PVC?
* Gentle and thorough shear: The biggest feature of the conical twin-screw extruder is the unique shape of screw. The feeding section has a large screw diameter and deep groove, which can easily "bite" fluffy powder and achieve forced feeding. As the screw diameter and groove volume gradually decrease, the material is strongly compressed. At the same time, the heater outside the barrel heats up, combined with the shear heat generated by the screw engagement, causing the material temperature to rise and melt and plasticize. The melted material is repeatedly stirred and sheared in the gap between the two screws, resulting in a more uniform mixture.
* Excellent mixing and degassing: Conical twin screw extruder can complete plasticization at relatively low temperatures, which is beneficial for volatile compounds to be fully extracted before being "locked" in the melt by high temperatures. In the exhaust section of the screw, the thread clearance is intentionally designed to be larger to increase the contact area with the exhaust port, allowing gas to be discharged more smoothly.
* Stable extrusion pressure: The design generates high and stable pressure, ideal for PVC melt extrusion through the die for preparation for pelletizing.
Stage 3: Air-Cooling Die Face Hot Cutting System
After the homogenized PVC melt leaves the extruder die, it enters the final stage: air-cooling die face hot cutting.
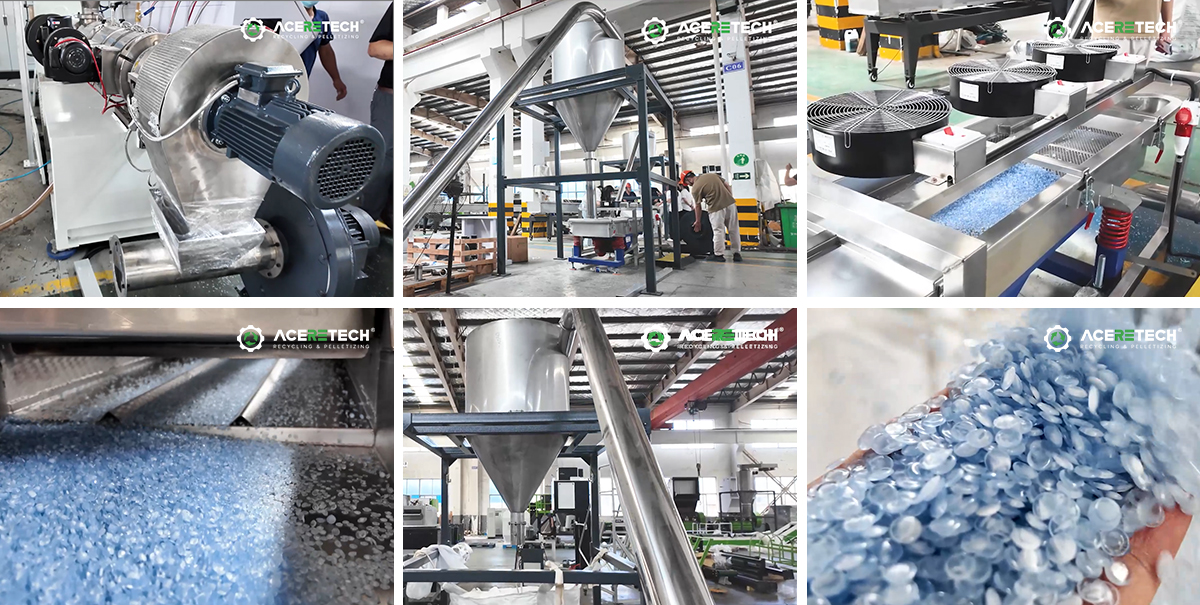
* Hot Cutting: Instead of cooling the molten material into strands and then cutting them (a slower process), it is cut directly on the die surface by a high-speed rotating knife. This results in perfectly shaped, smooth-edged, tailless spherical or "pillow-shaped" pellets.
* Cyclone silo: Hot cutted pellets are immediately enter into cyclone silo for cooling. Also, it uses centrifugal force to achieve air-solid separation. During rotation, PVC pellets with high density are subjected to strong centrifugal force and thrown towards the warehouse wall. Under the action of gravity, they slide down along the wall to the bottom conical hopper for collection. Clean waste air with low density forms an upward airflow in the center and is discharged from the top air outlet which takes away heat quickly. Generally, after being cooled by two cyclone silos, the material enters the vibrating screen and packaging system.
Conclusion: From Raw Material to Reliable Product
The entire process from PVC powder and additives to high-quality particles fully reflects advanced engineering design and process control level. It's a value-added transformation, transforming a commodity into a high-performance, reliable manufacturing product. By integrating a high-speed mixer, conical twin-screw extruder, and air-cooling hot-cut system, manufacturers can achieve higher quality, more efficient production, and more consistent product quality than simpler methods.
Investing in this integrated process goes beyond producing pellets; it lays the foundation for superior quality in all your PVC manufacturing. This solution ensures that every pipe, profile, and final component meets the highest performance and reliability standards, thereby gaining a significant competitive advantage for your business.
Click the link below to view a video on PVC powder pelletizing: